Interior and exterior trim is mainly plastic and thin-wall construction with many fastening points and high appearance requirements; lighting areas also involve the positioning accuracy of adjustment mechanisms and optical components.
Areas differ significantly in load mode, operating environment and failure consequences, so selection and process priorities also differ.
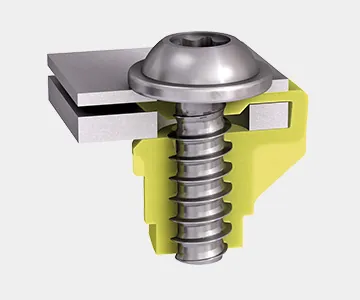
Grouped by joint type, each with a corresponding forming and surface treatment process route.
Used for plastic boss and trim panel fixing; thread profiles are designed to the plastic material and boss diameter, balancing joint strength and crack resistance.
Used for headlamp vertical and horizontal adjustment, with high requirements for thread accuracy, axial clearance and consistent feel.
Used for electronic modules, small trim parts and interior/exterior panels; small in size with large batch quantities.
The following are fastener types commonly used in this area, indicating the applicable product directions; for specific specifications and drawings, please submit them and an engineer will follow up.
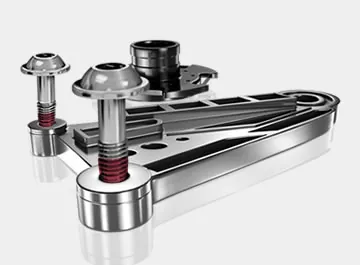
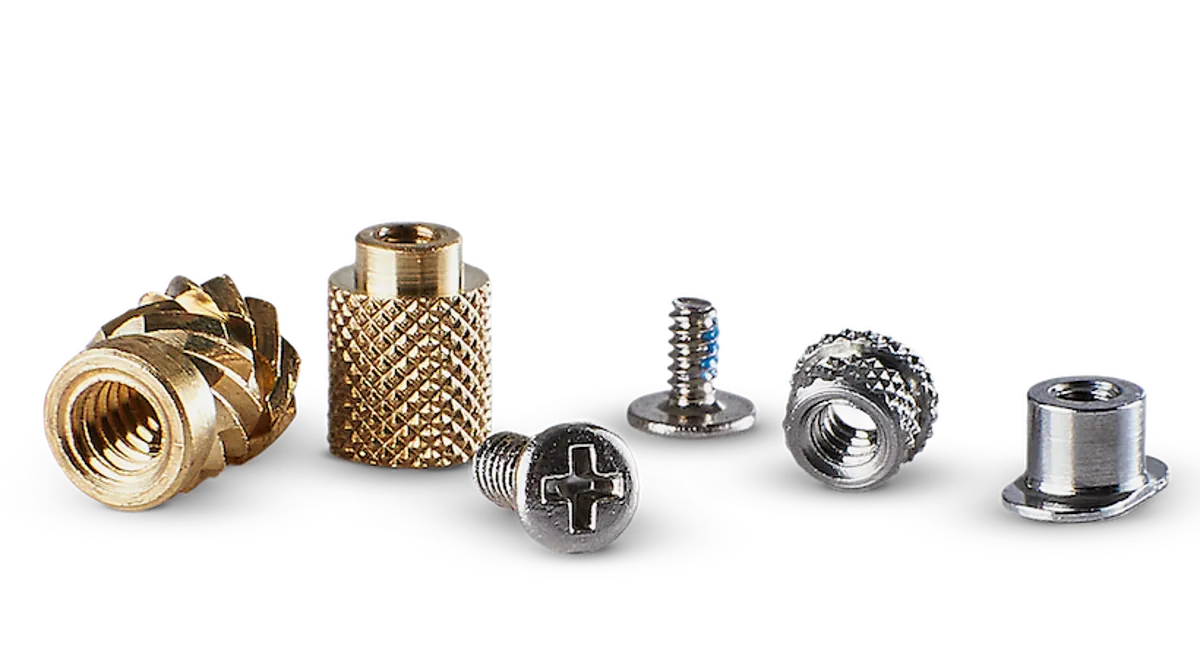
For an initial assessment of whether a requirement falls within the manufacturable range; specific solutions are subject to the drawing review conclusions.
| Item | Range and Notes |
|---|---|
| Common Sizes | Mainly M2 – M6; headlamp adjustment parts can be customised to drawing |
| Plastic Boss Suitability | Drive diameter calculated from boss diameter and wall thickness to avoid bursting or thread stripping |
| Assembly Cycles | Thread allowance and coating wear resistance designed to service and reassembly requirements |
| Surface Treatment | Mostly zinc or zinc-nickel plating, adjustable to plastic compatibility and appearance requirements |
| Appearance Control | For visible parts, burrs and coating uniformity are controlled to appearance standards |
| Packaging Format | Fixed-quantity packaging to assembly line requirements, reducing line-side sorting |
The following are the more common failure sources for this part category; they are identified and addressed before tooling.
Excessive drive diameter or an unsuitable thread profile causes plastic boss cracking; the profile must match the substrate and boss diameter.
Miniature parts have a narrow tightening window; the tightening tool and torque setting must be confirmed at the review stage.
Areas requiring repeated assembly should use wear-resistant coatings or structural anti-loosening solutions.
Flange bolts, bolts with captive washers, self-locking nuts, self-clinching fasteners and thread-forming screws.
Class 10.9 high-strength bolts, thread-forming screws, sealing plugs.
Self-clinching studs and standoffs, anti-loosening pre-applied adhesive bolts, sealing plugs and earth studs.
Precision miniature screws, sheet-metal self-clinching nuts and standoffs, panel fasteners.
Provide drawings and operating condition requirements; DFM review conclusions and optimisation proposals delivered within 3–5 working days.
